Manufacturing traceability

Mobile scanners for factory traceability

Mobile barcode, DPM, RFID and vision scanners for factory traceability, production data capture and MES/ERP workflows. Validate the exact device, application and station before deployment.

Plan a pilot

Outcome-led scope

Design the mobile workflow before locking the device SKU.

Manufacturing capture must work with difficult codes, gloves, noise, fixed stations, moving materials and production systems while preserving traceability through every exception.

  • Capture material and work-order events at the point of use
  • Improve traceability across production and quality steps
  • Select handheld, fixed, DPM or vision capture by station
  • Validate MES and ERP transactions before deployment

Priority workflows

Solution planning sequence

01

Material movement

Identify incoming material, line-side replenishment, WIP transfers and finished goods.

02

Production execution

Confirm work orders, components, routing steps and operator actions.

03

Quality and genealogy

Record inspections, nonconformance, rework and product history with reliable identifiers.

Solution planning sequence

Five service layers for a more predictable device program.

RuggedLayer organizes access to multiple manufacturers into a consistent engagement model. Each layer has a defined input, deliverable and evidence boundary.

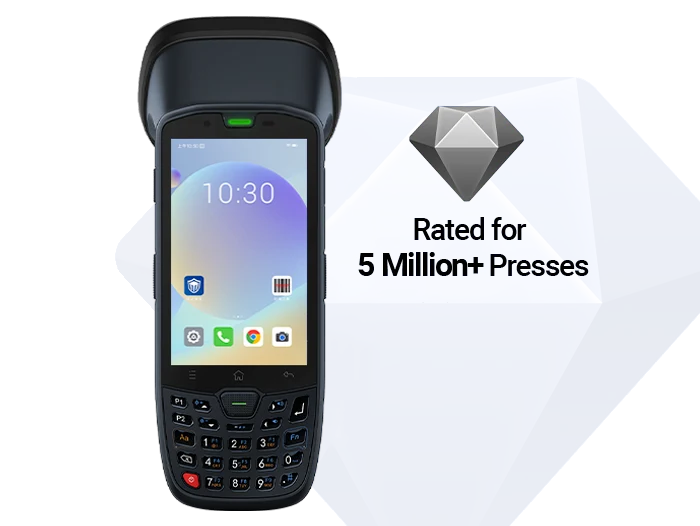
SEUIC AUTOID 10-DPM terminal for reading directly marked manufacturing codes
Code and station study

01 / Code and station study

Use the hardest marked code to define the capture method.

Manufacturing codes may be printed, laser marked, dot-peened or etched onto curved and reflective surfaces. Collect samples from normal production, rework and reject conditions. Record the size, contrast, material, distance, angle, lighting and line speed instead of describing every code simply as a QR code.

A DPM-capable reader is useful only when it reads the production mark repeatedly without slowing the station. Test the complete range of acceptable and marginal codes, then define what the operator does when a code cannot be read. Manual entry should be controlled and auditable rather than an invisible shortcut.

Outcome-led scope

  • Good, marginal and rejected code samples
  • Surface, lighting, angle and working distance
  • Read feedback in a noisy station
  • Controlled unreadable-code and manual-entry process
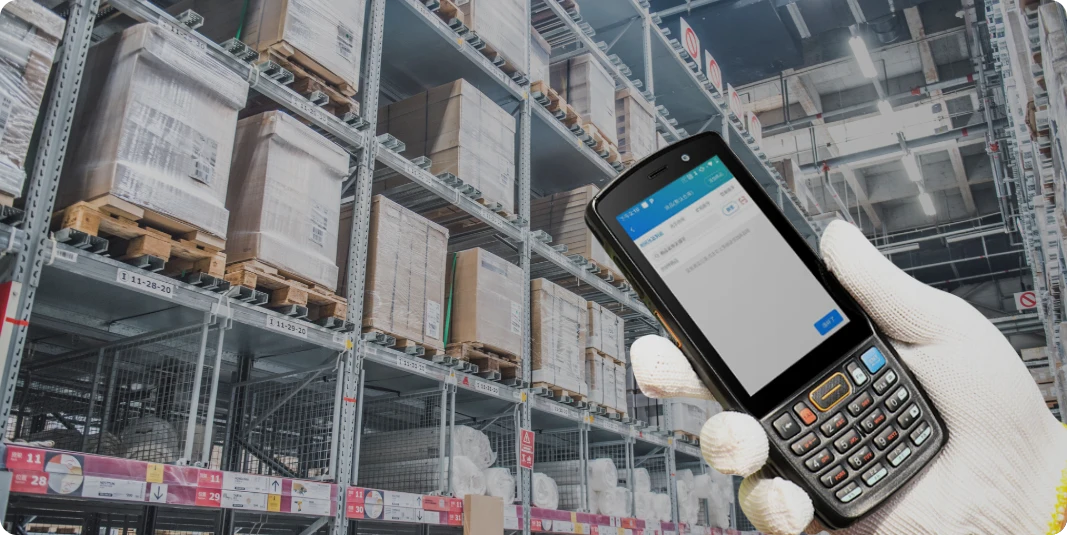
Goertek production and warehouse traceability workflow reference
Production traceability

02 / Production traceability

Connect each scan to a material, operation and result.

A scan by itself does not create genealogy. The MES or production application must know which work order, station, operator, component and operation the event belongs to. Define when the system validates before work, when it records completion and how it handles a component that belongs to another order.

Keep the screen focused on the current station. Operators need a clear pass, warning or stop response, plus a route for supervisor review. Synchronization should preserve event order and identifiers if the network is interrupted, because late or duplicated records can break the traceability chain.

Outcome-led scope

  • Work order, station and operator context
  • Component-to-product validation rule
  • Rework, scrap and supervisor override
  • Offline event order and duplicate protection
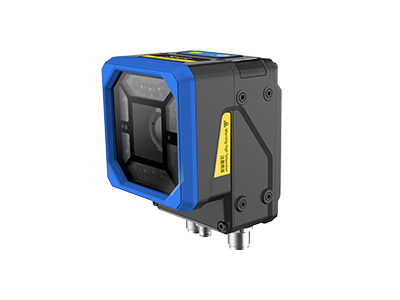
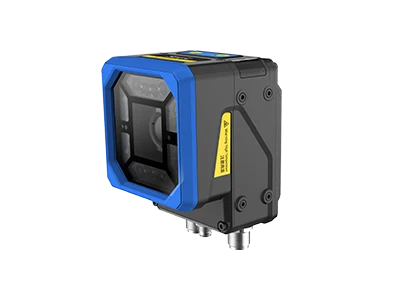
SEUIC X5 Pro visual reader as a fixed manufacturing capture option
Station rollout

03 / Station rollout

Approve a different physical setup where the work really differs.

A handheld may suit material movement while a fixed reader is better at a repetitive station. Vehicle mounts, tablets and wearable scanners solve other movement patterns. Standardization should reduce unnecessary variants without forcing one form factor into every job.

For each station type, document the reader, mount, cables or charging, host interface, software release and recovery owner. Run the pilot at production pace and measure first-read success, retries, cycle impact and operator intervention before purchasing at scale.

Outcome-led scope

  • Handheld versus fixed capture decision
  • Mount, cable, power and trigger arrangement
  • Production-rate repeatability test
  • Named ownership for support and change control
Priority workflows

Design the mobile workflow before locking the device SKU.

Code-specific capture

Test printed, etched, low-contrast, damaged and screen-based codes at the real station.

Industrial ergonomics

Match gloves, triggers, keypads, mounts and feedback to operator posture and task frequency.

System integration

Coordinate scan events, validation rules and error recovery with MES, WMS and ERP flows.

Environmental fit

Review dust, moisture, drops, temperature, ESD and cleaning requirements by work area.

Engineering and supply services

Five service layers for a more predictable device program.

  • MES, ERP, WMS and quality-management transactions
  • DPM, barcode, RFID and machine-vision capture
  • Workstation, vehicle, wearable and handheld form factors
  • Device management, firmware baseline and controlled application updates

Enterprise device portfolio

Mobile computers, barcode scanners and RFID readers by workflow.

A final shortlist depends on the application, scan or RFID workload, operating environment, country, deployment volume and support expectations.

UROVO DT40 keypad Android handheld computer for warehouse scanning

UROVO / Enterprise mobile computers

DT40

Keypad mobile-computer family for repeated industrial data capture.Devices
SEUIC AUTOID 10-DPM keypad handheld for direct part marking barcode capture

SEUIC (Dongji) / Keypad mobile terminals

AUTOID 10-DPM

DPM-oriented keypad terminal for demanding marked-code workflows.Devices
SEUIC X5Pro fixed industrial vision reader for high-speed barcode traceability

SEUIC (Dongji) / Visual readers

X5Pro

Visual reader option for code and inspection-oriented stations.Devices

Solution planning sequence

Plan a focused pilot.

  1. 01

    Select critical stations

    Prioritize difficult labels, high-frequency tasks and costly error paths.

  2. 02

    Build a capture matrix

    Record symbology, distance, lighting, surface, speed and host-system response.

  3. 03

    Run production trials

    Measure successful reads, retries, cycle impact and recovery behavior.

  4. 04

    Approve station standards

    Document device, mount, interface, software and support ownership for each station type.

RuggedLayer Test Lab

Plan a focused pilot.

Bring one workflow and its failure points; we will structure the device and test requirements.

Plan a pilot